Hardness Tester Indirect Verification: Close the Gap
Your hardness tester passed its annual verification — but did anyone check it since? Indirect verification against reference blocks keeps it audit-ready.
The hardness tester nobody put on the register
Halfway through a surveillance audit, the assessor walks into the metallurgy corner and puts a hand on the Rockwell machine. "Show me its calibration status." Dana, the quality engineer, pulls the certificate: a direct verification from an accredited lab, dated eighteen months ago, all in tolerance. The assessor nods, then asks the harder question. "And since then? What tells you it still holds tolerance today? Where are the reference blocks you check it against, and what’s their traceability?"
There is a drawer. In the drawer are three worn test blocks with faded certificates, none of them on the equipment register, none with a due date. The machine that decides whether a heat-treated part passes has been running for a year and a half on trust. That is the finding, and it writes itself.
Why hardness testers slip through the net
Most instruments announce their calibration status. A micrometer goes out to the lab, comes back with a sticker and a certificate, and lands on the schedule. A hardness tester behaves differently, and that difference is exactly why it disappears.
A hardness tester is verified in two distinct ways, and the standards are explicit about both. Direct verification checks the machine’s constituent parts — the test force, the indenter geometry, the depth-measuring system — usually annually or after any repair. It is the job you send out to an accredited lab. Indirect verification checks the machine as a whole by measuring certified reference test blocks and comparing the result to their certified value. Under ISO 6508-2 for Rockwell (and equivalently ASTM E18), indirect verification is required at defined intervals — commonly a daily routine check on each scale in use, plus a fuller periodic verification.
Here is the trap. Indirect verification happens in place, on the shop floor, performed by your own technician in a minute or two. Because nothing leaves the building and no external certificate arrives, the activity never gets treated as calibration. The tester slips off the register. So do the reference blocks — even though a certified reference block is itself a traceable measurement standard with its own certificate, its own uncertainty, and a finite working life. You end up with two classes of measuring equipment quietly governing your conformity decisions, and neither one is being managed.
ISO 9001:2015 clause 7.1.5.2 is not ambiguous here: monitoring and measuring resources used to verify conformity must be calibrated or verified at defined intervals against standards traceable to international or national standards, identified with their status, and safeguarded — with records retained. IATF 16949 and AS9100 flow the same requirement down with teeth. A hardness tester is a monitoring and measuring resource. Its reference blocks are the traceable standards. Both are in scope, full stop.
What indirect verification actually proves
It helps to see the measurement, because "we check it against a block" hides the real evidence.
Suppose the machine is used on the Rockwell C scale and you hold a reference block certified at 45.2 HRC, with a stated calibration uncertainty. The procedure is to make a short series of indentations — typically five — on the block, discard nothing arbitrarily, and compute two things. First, repeatability: the range of the five readings, which tells you whether the machine is stable. Second, error (bias): the difference between the mean of your readings and the block’s certified value, which tells you whether the machine is right. ISO 6508-2 gives the permissible limits for both, by scale and hardness level.
Run it and you might get a mean of 45.0 HRC with a range of 0.4 HRC — comfortably inside tolerance. Record it as the as-found condition. If it had come back at 43.1 HRC, you would have caught a machine that drifted low, quarantined it before it passed a batch of soft parts, sent it for direct verification and adjustment, and recorded the as-left value once it returned. That as-found/as-left pair is the whole point: it is the difference between "we think it’s fine" and "on this date, against this traceable block, it read this."
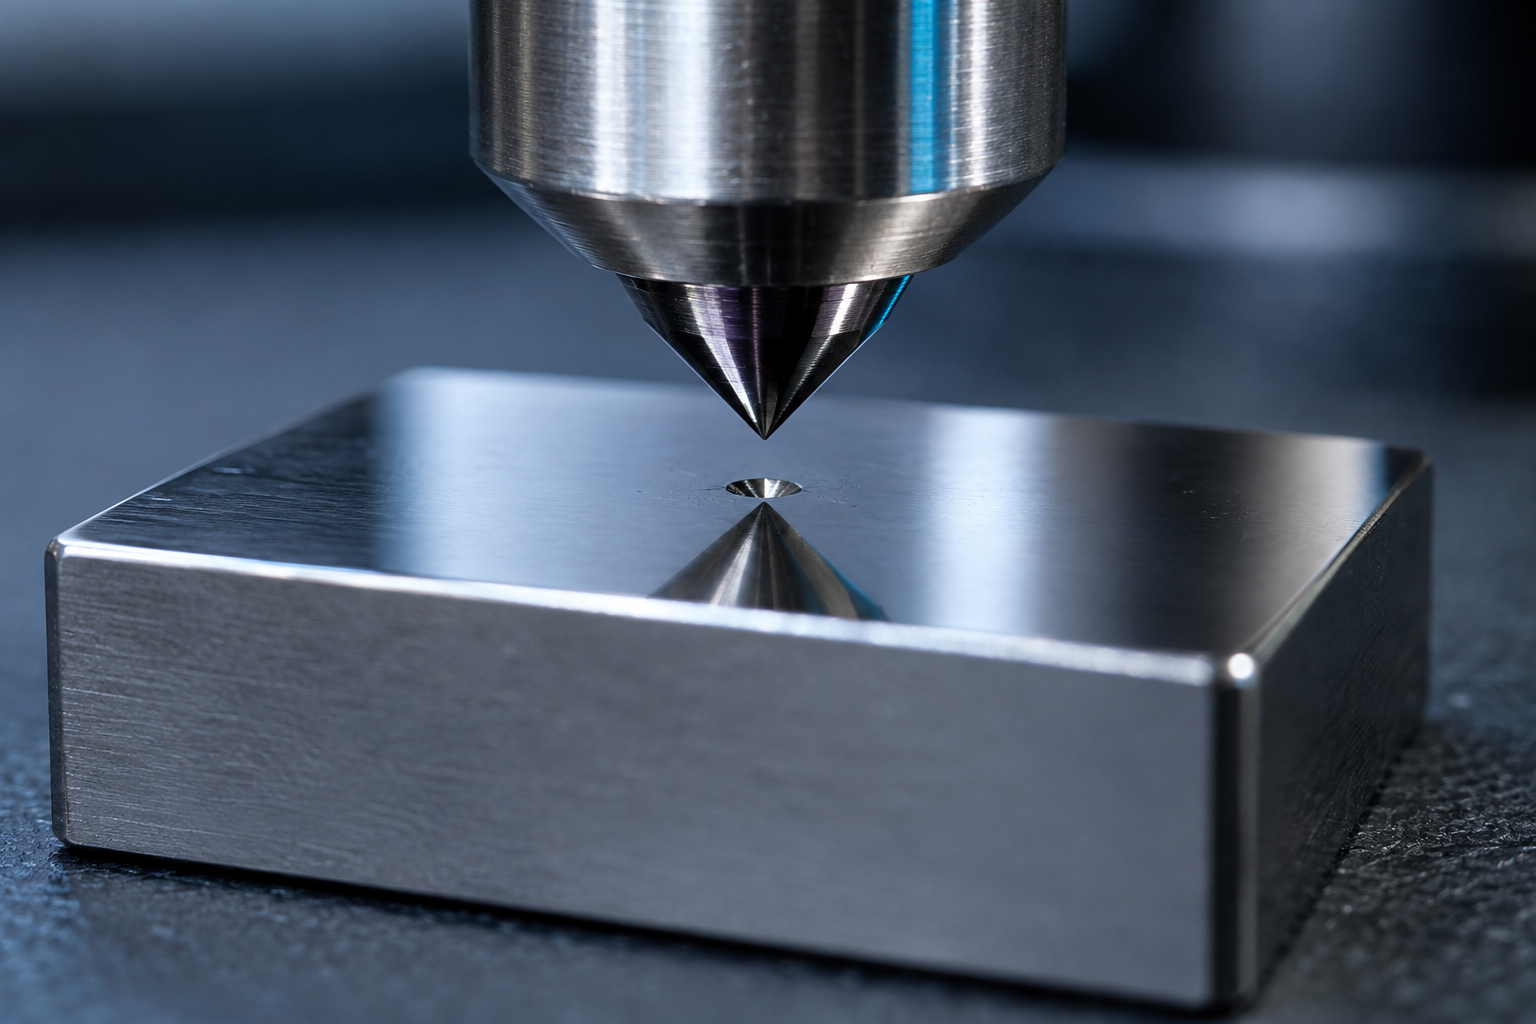
The reference block deserves the same discipline. A block is certified on specific faces and has a limited number of valid test points; standards and manufacturers cap its service life, and a block used past its validity — or worn on a face already covered in indentations — is no longer the standard you think it is. It needs a due date exactly as the machine does.
"Our lab does it annually — isn’t that enough?"
This is the objection every quality engineer raises, and it deserves a straight answer. No. The annual direct verification proves the machine was correct on one day. It says nothing about the 250 working days that follow, during which the indenter chips, the load cell drifts, or a bearing wears. Indirect verification is the interim evidence that the machine still holds tolerance between those annual events — and ISO 6508-2 requires it, so skipping it is not a shortcut, it is a nonconformity.
There is a second reason the auditor cares about the interval and not just the certificate: they read your record as a timeline. An eighteen-month gap with no interim checks tells them the machine could have been out of tolerance for over a year and you would never have known. A clean cadence of dated indirect verifications, each tied to a traceable block, tells them the opposite — that the measurement was under control continuously. Same machine, opposite audit outcome, decided entirely by whether the routine check was scheduled and recorded.
Getting the tester — and its blocks — under control
This is squarely the kind of shadow equipment a system like PrüfDesk exists to surface. Concretely:
- Register both, not just the machine. Enter the hardness tester and each certified reference block as instruments in their own right, with make, scale, certified value and uncertainty. The blocks stop living in a drawer and become tracked assets.
- Let due dates calculate themselves. Set the indirect-verification frequency on the tester and the recertification or validity limit on each block; PrüfDesk auto-calculates the next due date so neither can silently go overdue.
- Template the procedure once. Build a reusable indirect-verification procedure template — the five-indentation series, the repeatability and error checks against ISO 6508-2 limits, the as-found/as-left fields, the certificate upload — and apply it across every hardness tester of that type, overriding per unit where scales differ.
- Block use when it’s overdue. With configurable overdue blocking, a tester past its indirect-verification date can hard-block or soft-warn per your tenant’s policy, so a technician can’t unknowingly certify parts on an unverified machine.
- Keep the possession trail. Reference blocks get checked out and moved between machines; the allocation and location history records who held which block when — the traceability an auditor follows from a hardness reading back to the certified standard.
- Export the evidence. When the assessor asks the hard question, the answer is an audit-ready PDF: the tester’s verification history, every reference block’s certificate and due status, and the as-found/as-left records behind each check.
A short pre-audit checklist
- Is the hardness tester on the equipment register with a defined indirect-verification interval?
- Is every reference block registered, with its certified value, uncertainty and validity/due date?
- Do your routine checks record repeatability and error against the block’s certified value?
- Are as-found and as-left both captured when a machine is adjusted?
- Can you produce the interim verification timeline, not just last year’s direct-verification certificate?
- Does an overdue tester get blocked or flagged before it’s used?
If any line gives you pause, that is the gap an unannounced auditor will find first. Closing it doesn’t take a new machine — it takes putting the tester and its blocks on the register, scheduling the check the standard already requires, and keeping the record where you can hand it over. If you’d like to see how that looks in practice, register a single hardness tester and its blocks in PrüfDesk and run one indirect verification through the template. The next time someone puts a hand on the machine and asks, you’ll have the answer before they finish the question.