Bias & Linearity Studies: Control the Reference Master
A bias study is only as good as its reference value. What happens when the auditor asks for the setting ring's certificate on the study date?
Your Bias Study Is Only as Good as the Master Behind It
Sandra runs supplier quality for a machining plant that makes transmission housings. Her linearity study on the Ø22 mm bore gauge looked textbook: five reference parts spread across the operating range, twelve readings each, bias statistically indistinguishable from zero at every point, and a flat regression line. It went into the PPAP as part of element 8 without a second thought.
Eight months later the customer’s supplier quality engineer, working through a warranty return, asked one question: "Where do the reference values come from, and what was their calibration status on the day of the study?" The reference values had been assigned on the CMM in 2024. The master parts had sat in a drawer since then. Nobody could say whether the setting ring used to zero the gauge that week was the ring on the certificate or its twin from the second shift. The study wasn’t wrong. It just couldn’t be defended, and in an audit those two outcomes look the same.
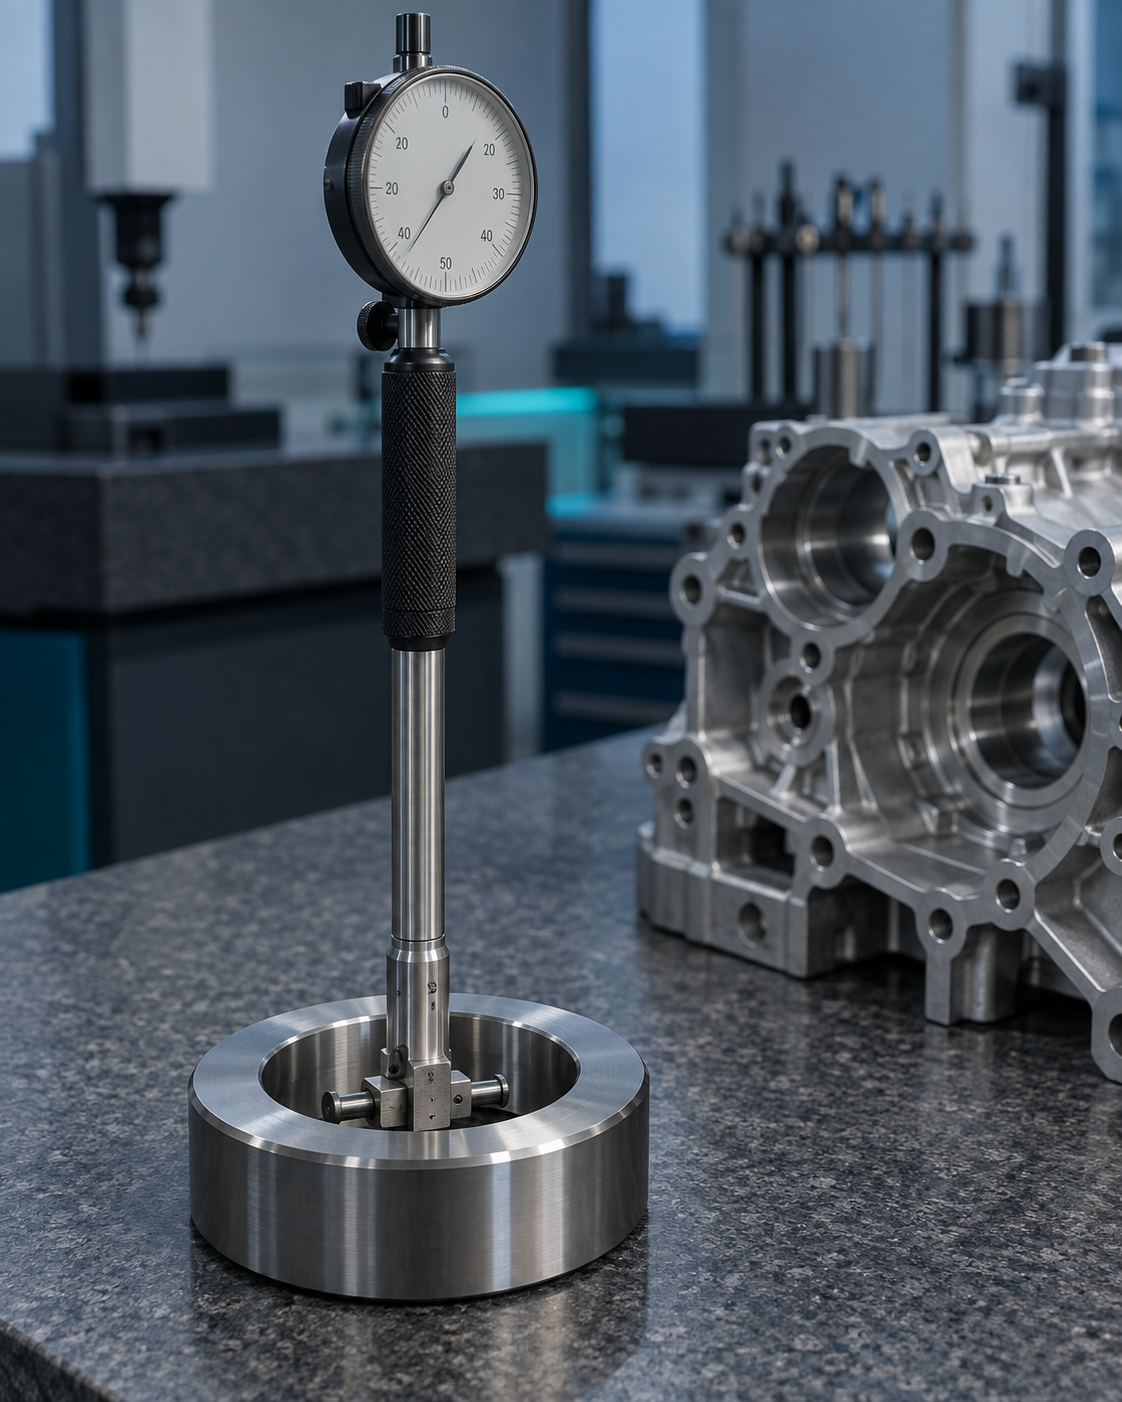
What bias and linearity actually measure
In the AIAG MSA reference manual (4th edition, still current), bias is the difference between the observed average of repeated measurements and a reference value for the same part. Linearity is how that bias changes across the gauge’s operating range. The usual approach is to pick at least five parts covering the range, assign each one a reference value, measure each part repeatedly (commonly ten or more times), and regress bias against reference value. You then test whether the bias line is statistically consistent with zero: slope, intercept, and the confidence band at each point.
The part that gets skipped is in that definition. Every bias figure is a subtraction, observed average minus reference value. The statistics can be flawless and still carry every error in the reference value, because bias is defined against the reference. If the reference value is wrong by 3 µm, the calculated bias is wrong by 3 µm. No test inside the study can detect that: the study assumes the reference is the truth.
That’s why the manual expects reference values to be determined with measurement equipment of higher order, such as a tool-room or layout measurement, a CMM, or a calibrated master. It’s also why IATF 16949:2016 doesn’t leave this to good intentions.
Where IATF 16949 puts the requirement
Clause 7.1.5.1.1 requires statistical studies on every type of inspection, measurement and test equipment system named in the control plan, with methods and acceptance criteria that conform to the customer’s reference manuals. Clause 7.1.5.2 requires measuring equipment to be calibrated or verified against standards traceable to international or national measurement standards, identified so its status can be determined, and protected from damage and deterioration that would invalidate the result.
Put the two together and the reference master is itself measuring equipment whose result your MSA depends on. A setting ring, a gauge block set or a set of CMM-assigned master parts that isn’t under calibration control is a gap in the traceability chain. It sits directly underneath a study you’ve submitted as PPAP evidence.
A worked example: 3 µm that nobody saw
Take Sandra’s bore. The tolerance is 22.000 ±0.015 mm, so 30 µm total. Her linearity study reports a maximum bias of +2 µm at the top of the range, with zero inside the confidence interval everywhere. That’s a clean result.
Now assume two things that happen in real plants:
- The setting ring has worn. It’s used at every shift start, and the as-found result at its next calibration shows the bore 3 µm over its certified size. The gauge was zeroed to the certified value, so every reading during the study was shifted by the same 3 µm.
- The master parts drifted. Their reference values were assigned on the CMM two years earlier. One part has a handling ding and light corrosion in the bore. Its real size is no longer the number written in the study spreadsheet.
The first error is a constant offset. It moves the whole bias line, and since the bias calculation assumed the ring was correct, it disappears into the result. The second is an error at one point only. It can create or hide a slope, and a slope is what the linearity study exists to find. Against a 30 µm tolerance, 3 µm is 10% of the tolerance band that nobody accounted for. That’s enough to change a conformity decision on parts near the limits, and enough for a customer to question every capability study that used the gauge.
The as-found result is what makes this visible. It also creates an obligation: under 7.1.5.2.1, when equipment is found out of calibration, you have to assess the validity of earlier measurement results, and that includes the MSA studies it supported.
The objection: "It’s a hardened steel ring. It doesn’t change."
Most of the time it doesn’t change much. But there are three problems with relying on that.
First, "much" is carrying the argument. Setting rings are used at every shift start, and repeated contact, handling and occasional drops are exactly how rings end up out of tolerance at calibration. Second, the standard doesn’t ask whether the ring is likely to be fine. It asks for evidence that it was traceable and in status when the result depended on it. Third, the auditor won’t argue about hardness. They’ll ask for the certificate and the due date, and they’ll check that the serial number matches what was on the bench.
The second objection is usually: "Our reference values come from the CMM, and the CMM is accredited-calibrated." Good, but that covers the CMM on the day it assigned the values. Master parts need their own identity, their own re-verification interval, and a record of which CMM calibration period their reference values came from. A reference value assigned in 2024 describes the part as it was in 2024.
Treat every reference master as a controlled instrument
This is where the equipment system matters. The bias statistics stay with the AIAG manual and your statistics tool; PrüfDesk doesn’t compute bias, linearity or %GRR. What it does is keep the reference masters under the same control as the gauges they validate:
- Register each master as its own instrument. Every setting ring, gauge block set and master part gets its own asset ID and serial number, and its own calibration due date calculated automatically from its interval. Record that ID in the study record, and the question "which ring?" has a one-line answer.
- Keep calibration records with as-found and as-left values. When a ring comes back 3 µm over, the as-found value is on file with the certificate. It’s the trigger to review the studies that relied on the ring, instead of something nobody finds.
- Use reusable procedure templates, overridden per unit where needed. One template covers all setting rings of a type. A ring that sees daily use can get a shorter interval or an extra check without splitting the whole family.
- Turn on hard overdue blocking for masters. Configure it so an overdue master can’t be checked out. Nobody zeroes a gauge for a study against a ring whose status lapsed last week.
- Rely on the check-out and possession trail. Who had the ring, and where, on the study date is recorded, which settles the "first shift or second shift ring" question with evidence.
- Produce audit-ready PDF reports. The master’s calibration history and certificates for the study period go into one document you can attach to the MSA file or hand to an auditor.
Checklist before your next bias or linearity study
- Every reference master (rings, gauge blocks, master parts) is registered with its own ID
- Each master was in calibration on the study date, and its certificate is on file
- Master-part reference values record which instrument assigned them, and when
- The master’s asset ID is written into the study record
- Overdue masters are hard-blocked from check-out
- The as-found history is reviewed before you reuse old reference values
The point
A bias study answers "how far is my gauge from the truth?" It can only do that if the truth is defensible. Keep the reference master under the same control as the instruments it’s meant to prove, and element 8 holds up when a customer asks where the numbers came from.
If you want to see how your current setting rings and master parts would look as registered, controlled instruments, PrüfDesk can walk through it with your own equipment list.